Printed circuit boards and their assemblies (PCB & PCBA) are the core components of electronic products, and their reliability directly determines the overall reliability of electronic products. To ensure and enhance the quality and reliability of electronic products, it is essential to carry out comprehensive physical and chemical analyses of failures, identify the underlying failure mechanisms, and then propose corresponding improvement measures. MTT possesses profound technical expertise in board-level failure analysis, a complete range of analytical methods, a vast database of case studies, and a team of experienced experts, providing you with high-quality and efficient failure analysis services.
The purpose of electronic component failure analysis is to employ a variety of testing and analytical techniques and procedures to identify the failure phenomena of electronic components, determine their failure modes and mechanisms, identify the ultimate root cause of failure, and propose recommendations for improvements in design and manufacturing processes. This helps prevent the recurrence of failures and improves the overall reliability of the components.
The continuous rise in complexity and performance requirements of integrated circuits, combined with potential risks across design, manufacturing, packaging, and application stages, has led to frequent occurrences of critical failure modes such as short circuits, open circuits, leakage, burnout, and parameter drift. These issues not only result in costly device scrapping and system downtime but also often trigger disputes over responsibility among designers, foundries, packaging and testing houses, and end-users, causing significant economic losses and reputational risks.
The performance requirements for polymer materials continue to rise, while differences in understanding of high-demand products and processes between customers and suppliers often lead to frequent failures such as fracture, cracking, corrosion, and discoloration. These failures frequently cause disputes over responsibility and result in significant economic losses.
The increasingly harsh service environments of metal components place higher demands on material performance and structural reliability. However, factors such as design flaws, material defects, manufacturing deviations, or improper use can readily trigger typical failures including fatigue fracture, stress corrosion cracking, hydrogen embrittlement, creep, wear, and overload deformation.
Didn't find what you were looking for?
Consult a professional engineer immediately for your service
Didn't find what you were looking for?
Consult a professional engineer immediately for your service
Meixin Testing leverages its technological edge in constructing massive failure databases, showcasing its capabilities through comprehensive case studies, solutions for complex scenarios, partnerships with leading enterprises, and systematic intellectual property. Drawing on millions of failure analyses, it delivers precise insights into root causes, enabling inspection reports to provide robust support for clients' quality upgrades and achieve zero failures.
Didn't find what you were looking for?
Consult a professional engineer immediately for your service
Stay updated with the latest news from Maxin Testing, including technical developments, exhibitions, and events. We build on a foundation of professional testing to deliver customized solutions for our clients, ensuring quality control from the source. This empowers our clients to stand out in the marketplace and achieve commercial success.
Didn't find what you were looking for?
Consult a professional engineer immediately for your service
MTT is a nationally accredited commercial third-party laboratory. We specialize in providing testing services, technical consulting services, and solution services to clients across industries including electronics manufacturing, automotive electronics, semiconductors, and aerospace materials.
Maxin Testing operates laboratory facilities in Shenzhen, Suzhou, and Beijing, featuring multidisciplinary testing and analytical laboratories. The company pioneers an industrial hospital service model grounded in materials science engineering and electronic reliability engineering.
Didn't find what you were looking for?
Consult a professional engineer immediately for your service
Professional verification platform, delivering precise data insights to build a solid foundation of trust for investors.
Didn't find what you were looking for?
Consult a professional engineer immediately for your service

Bright Lines on a Prism Film? Valley Cracking and Residual Isobornyl Acrylate in the Adhesive

Release date: 2026-11-20 13:42
Share to:

A batch of brightness enhancement film (prism film) developed local bright lines after die-cutting and baking. The bright area consisted of parallel bright stripes, with no visible bright lines above or below them. Films from the same batch without bright lines, and uncut raw material from an earlier batch, showed no such parallel stripes. The bright lines had a fixed direction that matched the periodic parallel prism structure, so the first question was whether the prisms had cracked, and where.

The measurements narrowed it down. The bright-line samples and the earlier raw material had the same prism dimensions, a pitch of about 50 μm and a height of about 25 μm, with the peaks intact. FTIR showed both adhesives were mainly polyacrylate. Cracking was concentrated at the prism valleys, the stress-concentration locations. The difference appeared one level deeper, at the monomer level: 300°C pyrolysis gas chromatography–mass spectrometry (Py-GC/MS) showed an extra peak at a retention time of 7.63 min in the bright-line sample, matched to isobornyl acrylate (IBOA), which the earlier raw material did not have. The unreacted monomer residue weakened the adhesive, the valleys tore under stress, and light leaked through the cracks as bright lines. The following five stages reconstruct the analysis: optical observation, morphology, cross-section, main-component comparison, and monomer comparison.

1. What the Bright Lines Look Like: Optical Observation

Method: The bright area of the sample was examined with a stereo microscope and compared with the earlier raw material.

Findings:

  • The bright area consisted of parallel bright stripes differing only in intensity, with no obvious bright lines above or below them.
  • No such parallel bright lines were visible on the surface of the earlier raw material.

Conclusion: The defect was not scattered bright spots but directional stripes aligned with the periodic prism structure. The problem lies in the prism structure and appears only in the batch that went through die-cutting and baking.

2. Cracks Open at the Valleys: Morphology

Method: Scanning electron microscopy (SEM) was used to examine the morphology of the bright-line region, together with the bright-line edge and a normal position.

Findings:

  • Bright-line region: no obvious cracking at the peaks; the valleys showed different degrees of cracking, some fully penetrated with wide openings, others not fully penetrated with a tearing pattern.
  • Bright-line edge: valleys were not fully cracked and the adhesive showed an outward tearing morphology; neither peaks nor valleys were cracked at the normal position.
  • Earlier raw material: no cracks at peaks or valleys, and no abnormality in the adhesive layer.

Conclusion: Cracking was concentrated at the prism valleys, the stress-concentration locations, with the peaks intact. The tearing pattern and outward pull of the adhesive indicate the adhesive itself was torn apart rather than the structure being broken by external impact.

3. FIB-Cut Valleys: Cross-Section Analysis

Method: Cross-sections of the bright-line position were prepared for microsection analysis, then a focused ion beam (FIB) was used to cut open the valleys of both the bright-line sample and the earlier raw material to compare the section morphology.

Findings:

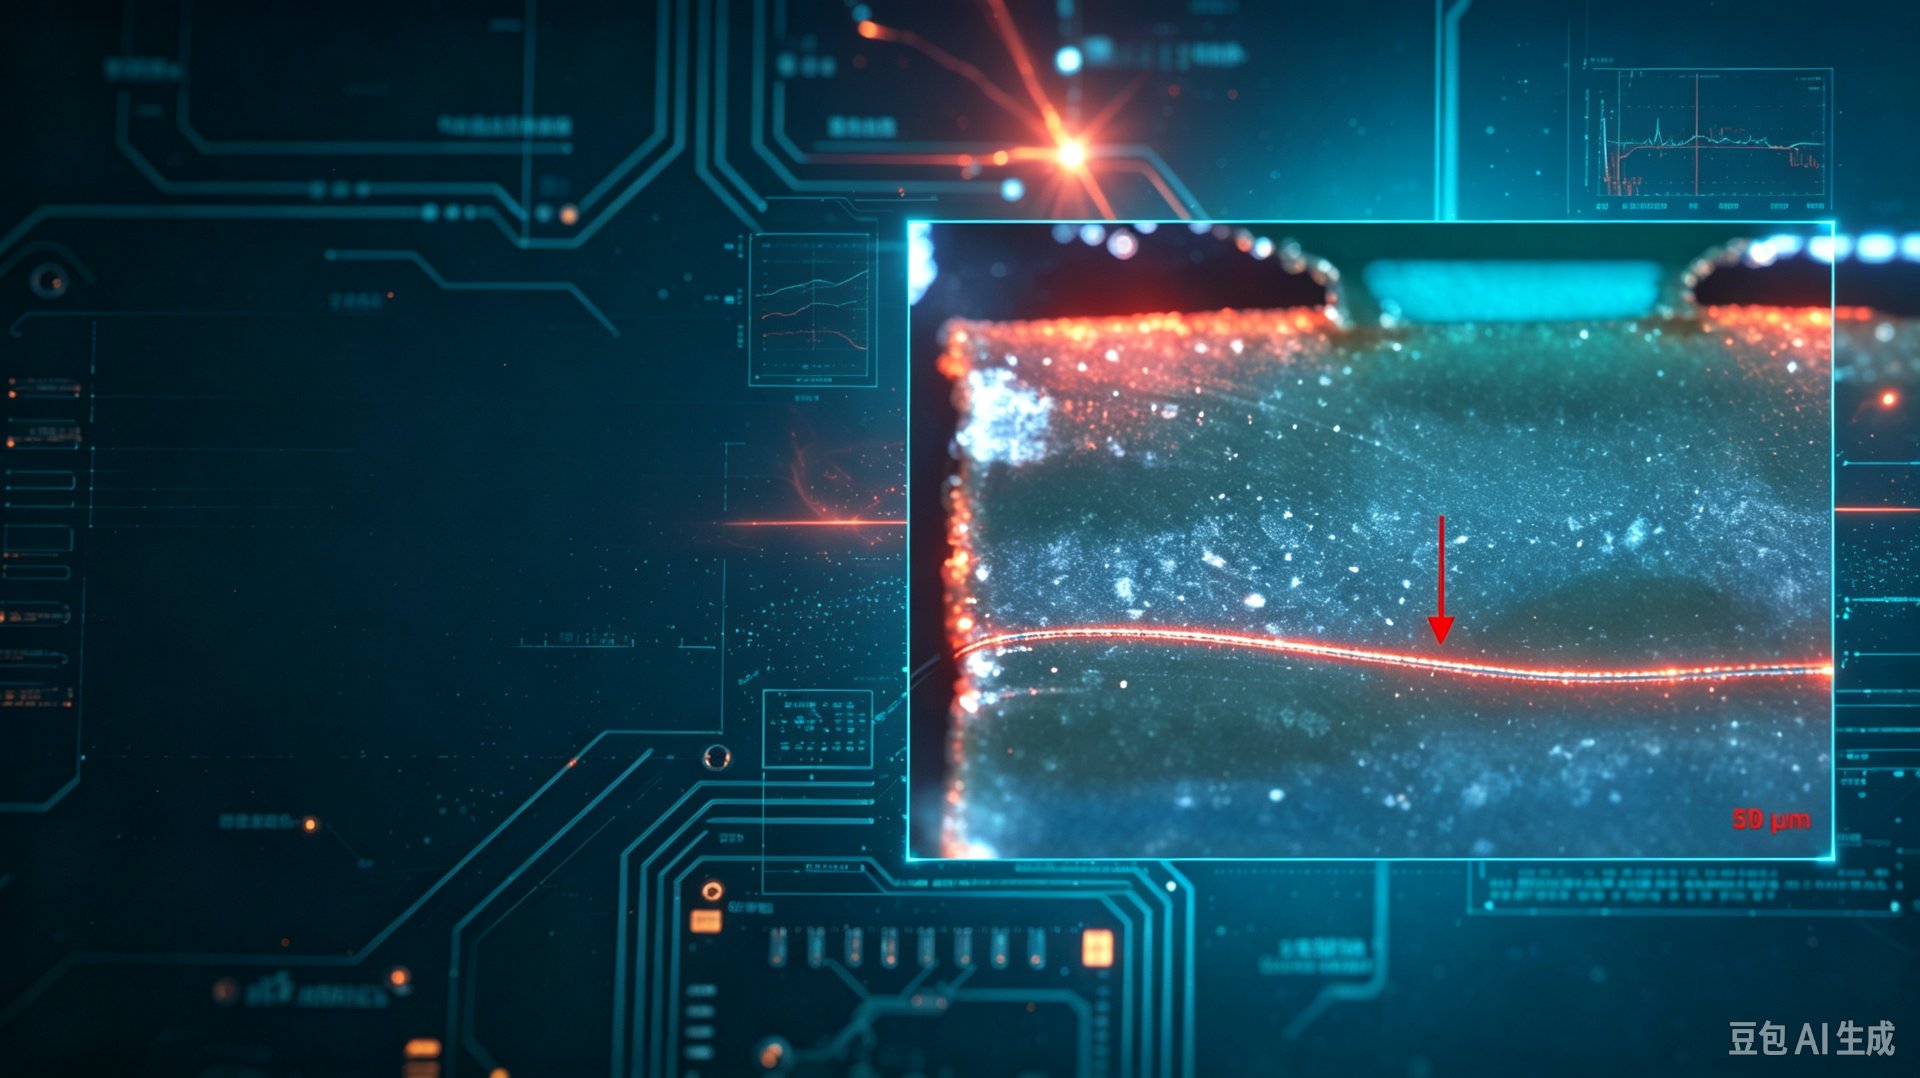
  • Cracking was not obvious in the prepared section because the mounting resin had entered the opened gaps. The bright-line sample and the earlier raw material showed no obvious difference in prism dimensions, with a pitch of about 50 μm and a height of about 25 μm.
  • Under FIB, the bright-line sample showed clear cracking at the valleys and stringing marks in the adhesive; the earlier raw material showed no obvious valley cracking.

Conclusion: Valley cracking is real, while the prism geometry is identical between the two batches. With structural dimensions matching, the problem points to the material itself and is unrelated to structural geometry.

4. Main Component of the Adhesive: FTIR

Method: Fourier-transform infrared spectroscopy (FTIR) was used to compare the adhesive composition of the bright-line sample and the earlier raw material.

Findings: The main components of the two were essentially the same, both polyacrylate. A small amount of PET was also detected, coming from the thin base film being scraped through during sampling, and is unrelated to the adhesive layer itself.

Conclusion: The bulk adhesive formulation had not changed. Since no difference appeared at the main-component level, the search moves to the finer monomer level to look for unreacted residue.

5. The Extra Peak: Py-GC/MS

Method: The bright-line sample and the earlier raw material were placed in pyrolysis cups and pyrolyzed at 300°C for compositional comparison.

Findings: The bright-line sample showed an extra chromatographic peak at a retention time of 7.63 min, matched to isobornyl acrylate. A second bright-line sample also contained isobornyl acrylate, while the earlier raw material had no such peak.

Conclusion: The adhesive of the bright-line film retained unreacted isobornyl acrylate monomer, the only compositional difference detected between the new and earlier batches. Detection in two bright-line samples and absence in the earlier raw material rule out single-point contamination or sampling chance.

Failure Mechanism

A brightness enhancement film concentrates light toward the front of the screen through a precise surface prism structure, and the prisms are fixed in shape by the adhesive layer. The bright lines came from a change in the adhesive composition: a relatively high amount of unreacted isobornyl acrylate reduced the strength of the adhesive. The prism valleys are stress-concentration locations, and after die-cutting and baking the added stress tore the adhesive at the valleys. Light then leaked directly through the cracks and appeared as parallel bright lines. Intact peaks, identical prism dimensions between batches, and the same polyacrylate main component exclude structural geometry and the bulk formulation, leaving insufficient adhesive strength from residual monomer as the cause.

Corrective Recommendations

The source report gives one improvement direction: strictly control the raw material ratio. Combined with the difference detected here, this breaks down into several actionable control points:

  • Control the monomer ratio and cure level. Unreacted isobornyl acrylate is the only compositional difference detected between the two batches, so the feed ratio and curing conditions are the first process parameters to review.
  • Include residual monomer in batch monitoring. 300°C Py-GC/MS can directly compare monomer differences between batches and can serve as a fixed tool for incoming material release or abnormal-batch investigation.
  • Run before-and-after controls on die-cutting and baking. The bright lines appeared only after these steps; retained samples from the same batch should be compared before and after processing to confirm the process window does not push valley stress beyond what the adhesive can withstand.
  • Keep retained samples of qualified batches. The monomer difference was identified only because earlier raw material was available for comparison; batch retention is a prerequisite for this kind of new-versus-old material comparison.

Disclaimer: This case has been desensitized. All data come from real laboratory analysis. Reproduction without permission is prohibited.
Relevant cases
How to Pinpoint PCB Leakage? Electrical Localization and Cross-Section Evidence of CAF
A power board leaked between connector pin1 and pin2. Visual inspection, X-ray and surface SEM/EDS showed no anomaly. Thermal EMMI localized a hotspot between the two through-holes, and cross-sectioning finally revealed a CAF filament with high Cu content inside a glass-fiber void. The root cause is copper ion migration along glass-fiber gaps under damp heat.
Why Did the Hardness of a Zinc-Aluminum Alloy Drop After Aging? Missing Solution Treatment and Overaging
A zinc-aluminum alloy phone cover aged at 120–220°C for 12 h without solution treatment saw hardness fall from 147 HV to 89 HV. Hardness, composition, metallography, SEM/EDS, and heat-treatment verification showed the root cause was missing solution treatment and excessive aging parameters. The peak hardness window is solution treatment followed by 100°C×50 min.
Exporting to California? A Practical Guide to Proposition 65 and Its Litigation Traps
California Proposition 65 (Prop 65) is a state-level statute and is not limited by product category, covering the entire supply chain. Its regulated substance list contains more than 960 chemicals known to cause cancer or reproductive toxicity, yet only about 300 have official safe-harbor thresholds. This article explains its scope, the exemption boundaries, and the two compliance routes for businesses.
Still failing despite meeting IPC standards? The OSP film thickness tolerance vulnerability overlooked by 90% of factories
After undergoing two reflow temperatures, OSP pads exhibited severe solderability issues during wave soldering. Reducing the reflow temperature resolved the solderability problems. This paper analyzes the failure causes and mechanisms of solderability defects on OSP pads and proposes improvement recommendations.
The Truth Behind the 30% Surge in FPC Lead-Free Failure Rates | The “Invisible Killer” of Consumer Electronics
A certain FPC exhibited routing shallowing at certain locations, with both the edges and central areas of the defective samples showing this phenomenon. This paper will conduct a systematic failure analysis to identify the root cause of routing shallowing in the FPC.
Silicone Exceeding Limits = EU Sales Ban? With Global Regulations Tightening, Is Your Product Compliant?
Siloxanes are a class of organosilicon compounds containing Si-O-Si bonds, widely used in rubber, detergents, polishes, adhesives, sealants, and other fields. Due to the environmental and health risks associated with certain siloxanes, numerous countries and regions worldwide have enacted regulations to control their use.
Email
marketing@mttlab.com
Business Consultation
Free Consultation
Report Inquiry
Back to Top
Contact Us
  • *Name:
  • *Contact:
  • *Email:
  • *Company/Organization/school:
  • *The location:
  • *Message information: